[email protected] Citar


[email protected] Citar
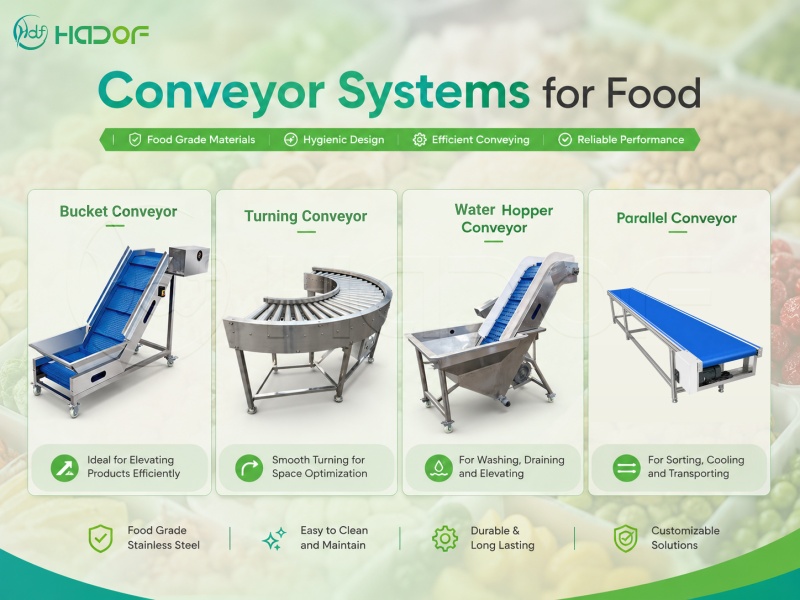
Food manufacturers need stable conveyor systems for food production, lavar, cooling, and packaging processes. Além disso, modern food factories require efficient material handling equipment with hygienic structure and flexible production design. Portanto, many customers search conveyor systems for sale before expanding food processing capacity.
Enquanto isso, fábricas de alimentos congelados, vegetable processing plants, and snack food manufacturers all face labor and space pressure. Consequentemente, they prefer automated food conveyor machinery with cost-effective investment and stable conveying performance. Nossa empresa provides customized food conveyor solutions for different food manufacturing procedures and production requirements.
Different food processing procedures require different conveying technology and production line design. Além disso, customers usually focus on processing capacity, factory layout, conveyor price, and maintenance cost before purchase decisions.

Elevator conveyor systems support vertical conveying and large height difference transportation. Além disso, this conveyor equipment handles granules, snack bags, vegetable materials, and packaging trays efficiently. Many potato chips production lines and vegetable washing lines use elevator machinery for automatic feeding procedures.
Além disso, our elevator conveyor adopts food-grade PU belts and stainless steel structure. Portanto, customers receive hygienic food handling performance and stable continuous conveying results. Enquanto isso, quick-disassembly structure reduces conveyor cleaning management cost. You’d better choose this conveyor machine when manual feeding increases labor investment.
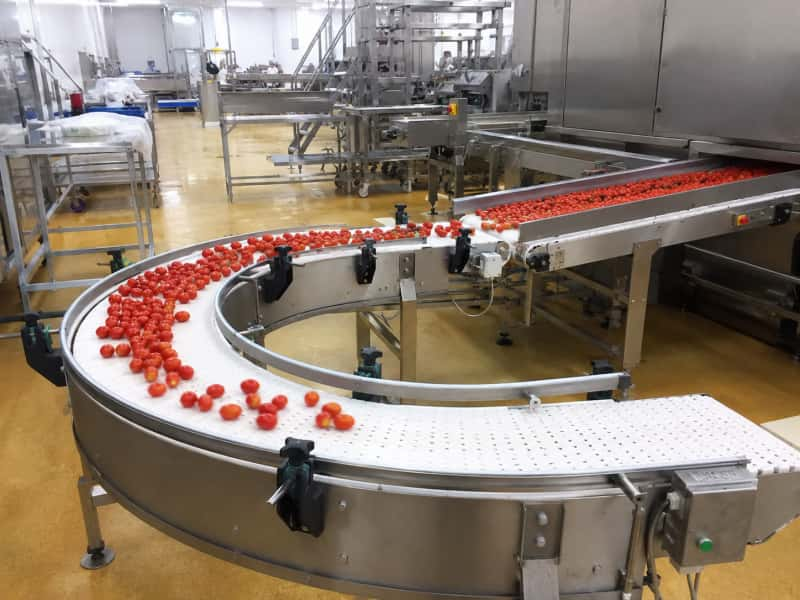
Turning conveyor systems solve food production line direction changing problems effectively. Além disso, this conveying equipment supports 90-degree and 180-degree turning process design. Many snack food factories and food packaging plants use turning conveyors in limited workshop areas.
Adicionalmente, our turning conveyor machinery combines arc belt technology and stable transmission systems. Portanto, clients improve workshop space utilization and production process connection efficiency. Why not try modular conveyor equipment when your factory needs L-shape or U-shape production layout?
Portanto, our engineers analyze raw material conditions and production workflow carefully.
Different food products require different conveying treatment and production management solutions. Enquanto isso, customers often compare conveyor quotation, operating cost, and long-term maintenance budget carefully. Portanto, our company designs customized conveyor systems according to food processing technology and product condition.
Water bucket conveyor systems combine water washing, cooling, lifting, and conveying functions together. Além disso, this conveyor equipment suits fruit processing, seafood treatment, and prepared vegetable manufacturing procedures. Many frozen food processing factories use this machine after blanching and frying processes.
Além disso, stainless steel water circulation systems improve food cleaning performance and cooling efficiency. No entanto, customers should arrange regular cleaning and disinfection management for water tanks and pipelines. Our engineers usually recommend this conveyor machinery for vegetable cleaning production lines and seafood processing systems.
Leia mais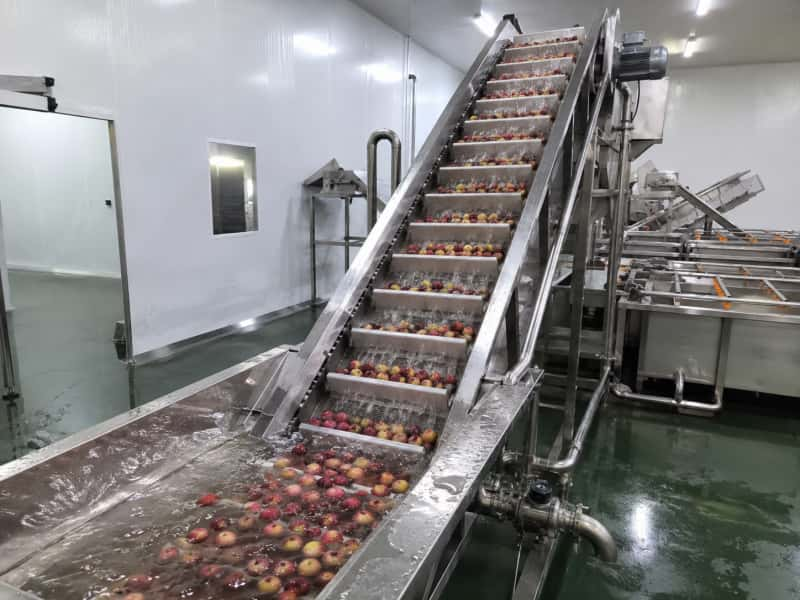
Parallel conveyor systems support multi-channel food conveying, cooling, buffering, and packaging procedures. Além disso, this conveyor equipment handles packaged snacks, bottles, bandejas, and fried food products continuously. Many baking production lines and frying food manufacturing plants prefer parallel conveyor technology.
Adicionalmente, modular mesh belt structure improves cooling process and product distribution efficiency. Portanto, customers increase packaging productivity and reduce production waiting time. Our company also provides customized conveyor width, belt quantity, and conveying speed adjustment solutions.
Leia mais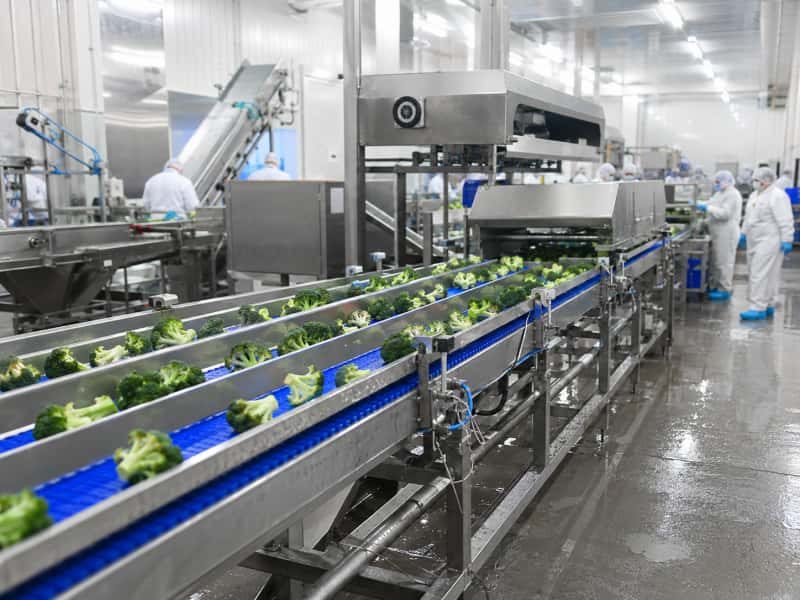
Food factories usually compare conveyor structure, cleaning difficulty, and production application before equipment purchase. Além disso, customers evaluate conveyor quotation and maintenance budget during food production line planning. Portanto, our engineers provide targeted conveyor system recommendations according to food processing technology.
| Conveyor Type | Main Function | Suitable Food Materials | Typical Production Position | Main Advantage |
| Elevator Conveyor | Vertical lifting and feeding | Granules, snack bags, vegetable pieces | Feeding section and high inlet position | Reduces labor feeding cost |
| Turning Conveyor | Direction changing | Packaged foods, bandejas, boxes | Compact workshop corners | Improves factory layout utilization |
| Water Bucket Conveyor | Lavando, cooling, lifting | Vegetais, frutos do mar, prepared foods | Cleaning and cooling process | Combines washing and conveying |
| Parallel Conveyor | Multi-lane conveying and cooling | Fried foods, bakery products, bottles | Cooling and packaging lines | Supports high-capacity production |
Além disso, many customers combine several conveyor machines into one automatic food processing system. Portanto, integrated conveyor production lines improve food manufacturing efficiency and reduce manual material handling pressure.
Food manufacturers usually evaluate conveyor system price, processing capacity, and factory expansion plans together. Além disso, export food factories focus on stainless steel material, CE certification, and hygienic conveyor design before equipment purchase.
Enquanto isso, our company provides customized food conveyor quotation according to processing technology and factory layout requirements. Single conveyor machine investment remains affordable for medium food factories. Complete conveyor production line systems also support long-term automatic food manufacturing development.
Finalmente, conveyor systems for food improve production efficiency, material handling management, and factory automation performance significantly. Portanto, many global food manufacturers continue purchasing intelligent conveyor equipment for modern food processing production lines.
Many food factories face labor feeding pressure and large height difference during food production procedures. Portanto, elevator conveyor systems become the preferred solution for automatic feeding management.
Além disso, customers can choose cleated belt structure or bucket elevator design according to material condition. These conveyor machines handle granules, vegetable pieces, snack foods, and small packaging bags efficiently. You’d better select elevator conveyor equipment for continuous food production lines with vertical conveying demand.
Some food processing plants have limited workshop space and complicated production line direction requirements. Portanto, turning conveyor systems support better food production layout management.
Além disso, turning conveyor machinery combines with straight conveyor equipment easily. Consequentemente, food factories create L-shape, U-shape, and circular production line layouts efficiently. Many snack food manufacturers and packaging factories improve workshop space utilization through turning conveyor technology.
Many fruit processing factories and seafood manufacturers require washing, cooling, and conveying functions together. Portanto, water bucket conveyor systems become a cost-effective food processing solution.
Além disso, this conveyor machinery combines water washing, cooling, lifting, and conveying procedures in one integrated system. Consequentemente, customers reduce equipment investment and production management complexity. Many vegetable processing plants and prepared food factories prefer this conveyor equipment after blanching and frying procedures.
Large food manufacturing plants usually require multi-channel conveying, cooling, buffering, and packaging procedures. Portanto, parallel conveyor systems support high-capacity food processing management effectively.
Além disso, multi-lane mesh belt conveyors improve cooling efficiency and packaging workflow connection. Consequentemente, fried food factories and baking production plants increase production efficiency significantly. Why not try parallel conveyor machinery when your factory needs multi-line packaging or cooling systems?
Deixe sua mensagem
 Orçamento Gratuito
 Português do Brasil
 English
 Afrikaans
 Shqip
 العربية
 Հայերեն
 Azərbaycan dili
 Беларуская
 Bosanski jezik
 Български
 မြန်မာစာ
 Hrvatski
 Čeština
 Dansk
 Nederlands
 Eesti keel
 Wikang Filipino
 Suomi
 Français
 Galego
 Deutsch
 Ελληνικά
 हिन्दी; हिंदी
 Magyar
 Íslenska
 Bahasa Indonesia
 Gaeilge
 Italiano
 日本語
 Қазақ тілі
 한국어
 ພາສາລາວ
 Latīna
 Latviešu valoda
 Bahasa Melayu
 Монгол
 नेपाली
 Norsk
 Português Português do Brasil
 Română
 Русский
 Cрпски језик
 Slovenčina
 Slovenščina
 Español
 Svenska
 ภาษาไทย
 Türkçe
 Українська
 Oʻzbek tili
 Tiếng Việt
Você não pode copiar o conteúdo desta página